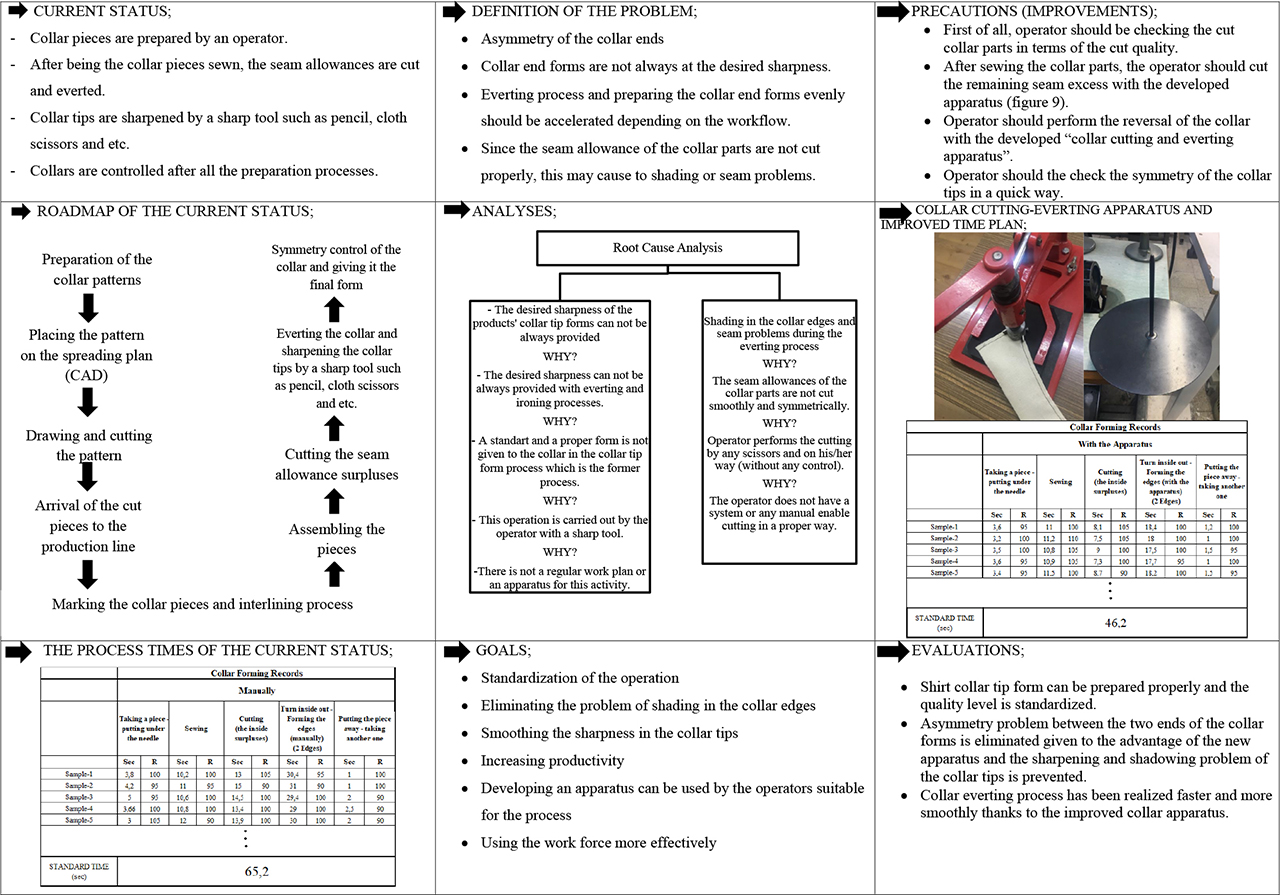
Table 1
The faults and effects
| FAULT | EXPLANATION | EFFECT | |
|---|---|---|---|
| 1. | Size difference | A difference in the size of the pieces | Repetition of the spreading-cutting processes |
| 2. | Barcode | The attached barcode does not belong to the product. | The delivery of the product to a different warehouse |
| 3. | Fabric Fault | Defects on the fabric affect the quality of the product | Disassemble process, repetition of the spreading-cutting processes |
| 4. | Button | Broken, incorrect, unsewn or improper positioning of the buttons | Disassemble process or re-sewing, productivity loss |
| 5. | Label | Incorrect, defected or incorrect positioning | Disassemble process and re-sewing, productivity loss |
| 6. | Needle | Unsuitable needle for the fabric or the yarn | Damage to the product, re-cutting and re-sewing processes, fabric waste, cost increase |
| 7. | Button hole | Unsuitable position, number or type | Damage to the product, re-cutting and re-sewing processes, fabric waste, cost increase |
| 8. | Yarn | Yarn knitting, knotting or fringing | Loss of productivity and quality |
| 9. | Seam Fault | Seam faults, such as skipping or disassembling | Re-sewing, loss of productivity and time |
| 10. | Stain | Colour changes occurred on the product due to various reasons | Loss of productivity and time |
| 11. | Cuff form | Position, sewing, ironing or size-related defects | Labour, time and productivity loss |
| 12. | Position | Not settling the product pieces at specified lines or levels | Labour, time and productivity loss |
| 13. | Colour difference | Colour mismatch between product parts | Productivity loss, re-cutting and re-sewing processes, fabric waste, cost increase |
| 14. | Disassembly | Stitch defect between parts, button, buttonhole and hemline | Labour, time and productivity loss |
| 15. | Fibre flies | Adhesion of fly fibers on the products | Productivity loss |
| 16. | Interlining resin traces on fabric surface | Non-sticking or -tracing the interlining resin on the fabric surface | Labour, time and productivity loss |
| 17. | Collar tip form | Wrong positioning of the collar and visible seam allowance | Productivity loss |
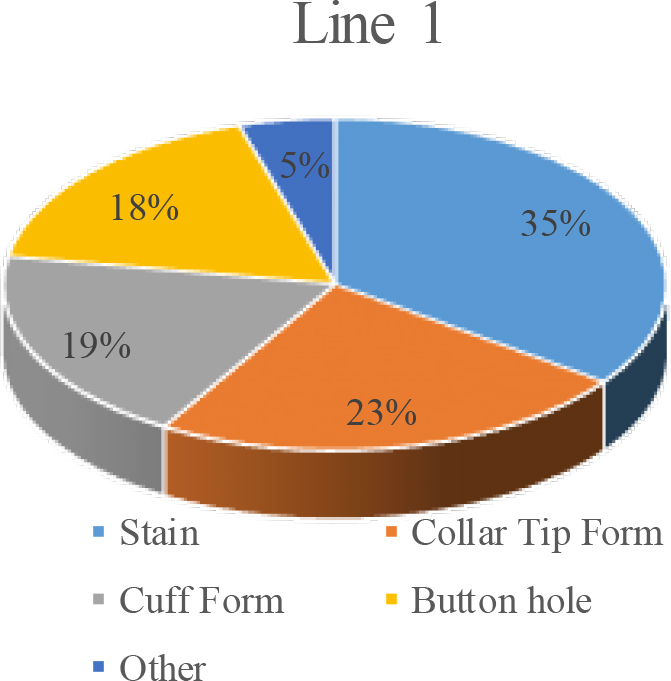
Fig. 1
Faults of line-1
→ Data obtained from Line-1
- Daily average checked quantity: 504
- Number of working days: 22
- Total number of controls during the working time: 11.088
- Total number of faults encountered: 640
- Fault type and frequency
o Stain à 224
o Collar Tip Form à 151
o Cuff Form à 122
o Button hole à113
o Other à 30
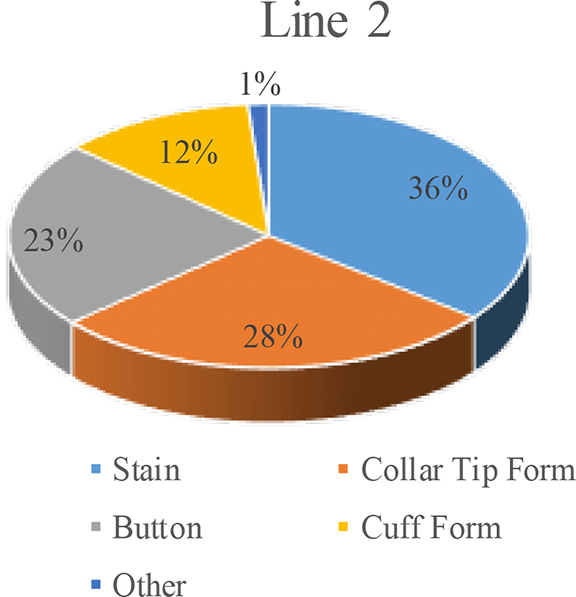
Fig. 2
Faults of line-2
→ Data obtained from Line-2
- Daily average checked quantity: 1000
- Number of working days: 22
- Total number of controls during the working time: 22.000
- Total number of faults encountered: 1536
- Fault type and frequency
o Stain à 547
o Collar Tip Form à 430
o Button à 354
o Cuff Form à 185
o Other à20
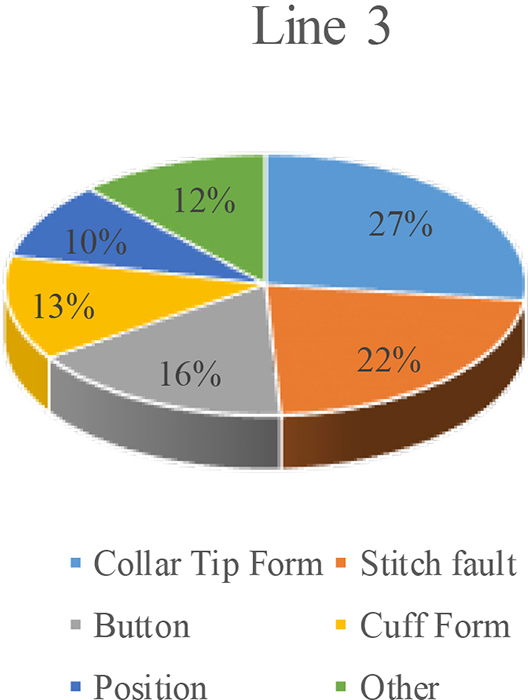
Fig. 3
Faults of line-3
→ Data obtained from Line-3
- Daily average checked quantity: 1200
- Number of working days: 22
- Total number of controls during the working time: 26.400
- Total number of faults encountered: 2115
- Fault type and frequency
o Collar Tip Form à 570
o Stitch fault à 468
o Button à 348
o Cuff Form à 274
o Position à 204
o Other à 251

Fig. 4
Faults of line-4
→ Data obtained from Line-4
- Daily average checked quantity: 950
- Number of working days: 22
- Total number of controls during the working time: 20.900
- Total number of faults encountered: 1210
- Fault type and frequency
o Stain à 374
o Collar Tip Form à 371
o Cuff Form à 258
o Interlining Resin à 177
o Other à 30
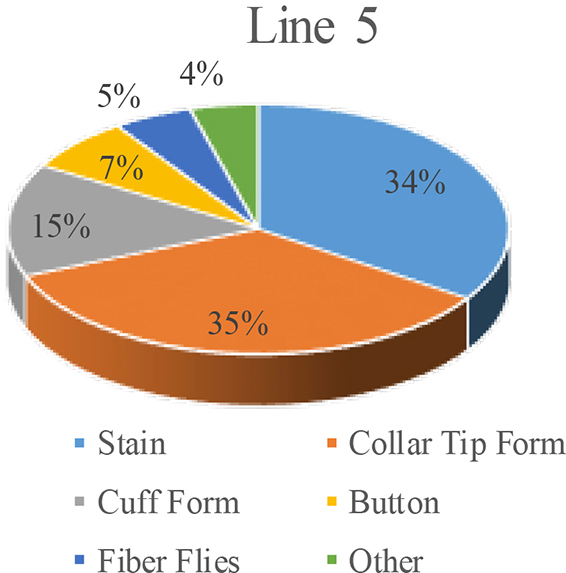
Fig. 5
Faults of line-5
→ Data obtained from Line-5
- Daily average checked quantity: 1000
- Number of working days: 22
- Total number of controls during the working time: 22.000
- Total number of faults encountered: 1974
- Fault type and frequency
o Collar Tip Form à 681
o Stain à 678
o Cuff Form à 289
o Button à138
o Fiber Flies à 101
o Other à 87
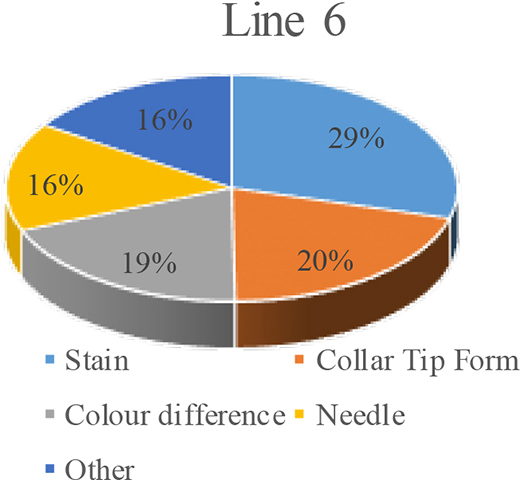
Fig. 6
Faults of line-6
→ Data obtained from Line-6
- Daily average checked quantity: 1150
- Number of working days: 22
- Total number of controls during the working time: 25.300
- Total number of faults encountered: 1210
- Fault type and frequency
o Stain à 355
o Collar Tip Form à 247
o Colour Difference à 231
o Needle à 188
o Other à 189
Table 2
Faults and their frequency
| Fault | Fault quantity | Fault percentage (%) | Cumulative percentage (%) | |
|---|---|---|---|---|
| 1. | Collar Tip form | 2450 | 28,21 | 28,21 |
| 2. | Stain | 2178 | 25,08 | 53,29 |
| 3. | Cuff Form | 1128 | 12,99 | 66,28 |
| 4. | Button | 870 | 10,02 | 76,30 |
| 5. | Seam Fault | 468 | 5,39 | 81,69 |
| 6. | Needle | 248 | 2,86 | 84,55 |
| 7. | Color Difference | 231 | 2,66 | 87,21 |
| 8. | Position | 206 | 2,37 | 89,58 |
| 9. | Interlining Resin | 177 | 2,04 | 91,62 |
| 10. | Fiber Flies | 152 | 1,75 | 93,37 |
| 11. | Button Hole | 113 | 1,30 | 94,67 |
| 12. | Yarn | 103 | 1,19 | 95,86 |
| 13. | Size Difference | 100 | 1,15 | 97,01 |
| 14. | Fabric Fault | 89 | 1,02 | 98,03 |
| 15. | Label | 87 | 1,00 | 99,03 |
| 16. | Barcode | 45 | 0,52 | 99,55 |
| 17. | Disassembly | 40 | 0,46 | 100 |
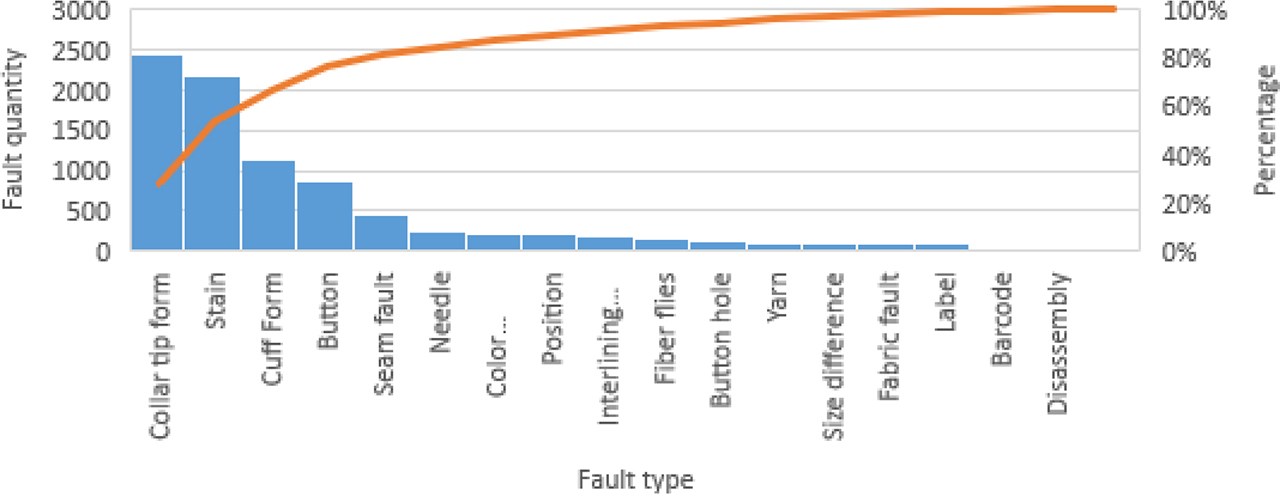
Fig. 7
Pareto diagram of the faults
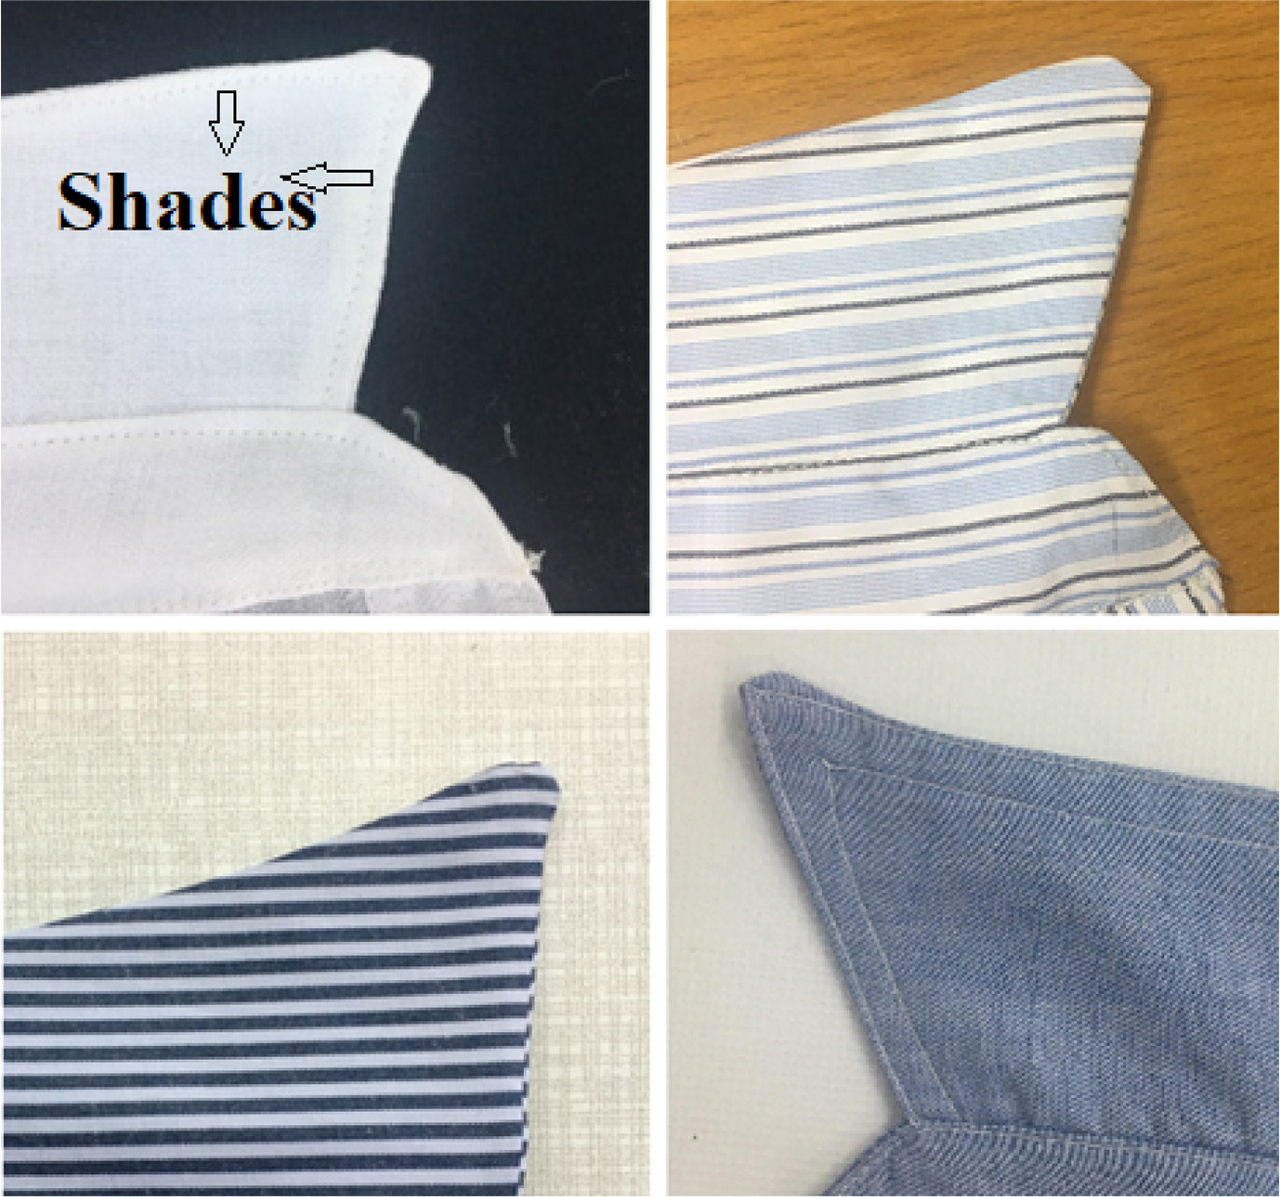
Fig. 8
Samples of 2nd quality collars
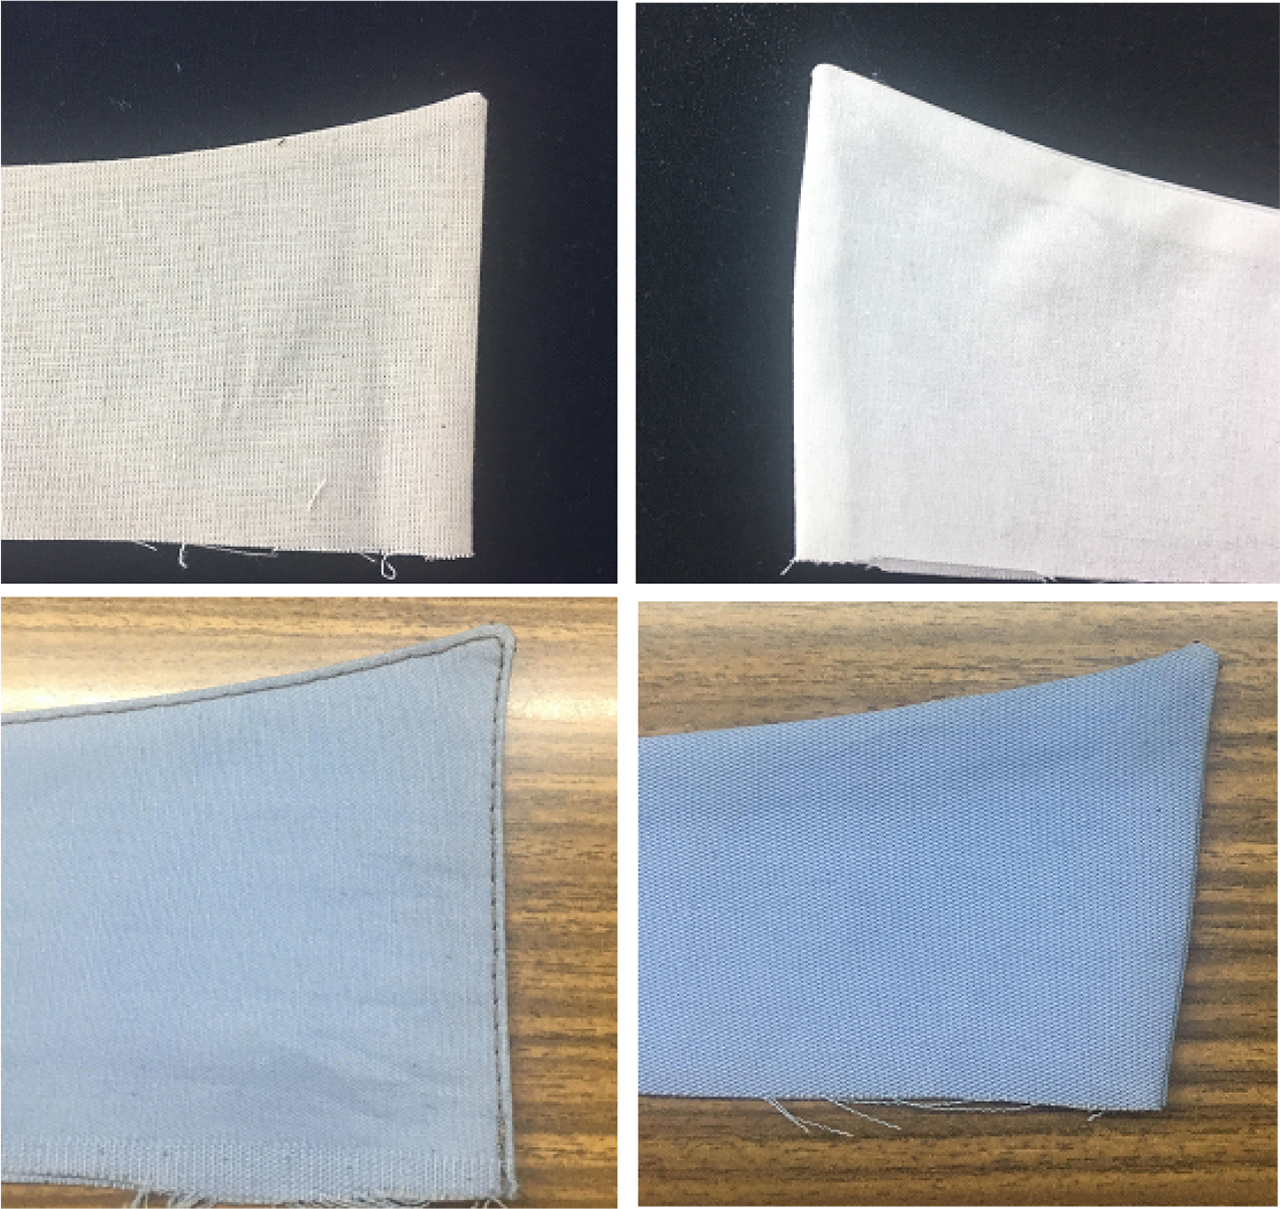
Fig. 9
Collars manufactured with the apparatus
Table 3
Records obtained by manual processes
| Collar Forming Records | ||||||||||
|---|---|---|---|---|---|---|---|---|---|---|
| Manually | ||||||||||
| Taking a piece - putting under the needle | Sewing | Cutting (the seam allowance) | Turn inside out - Forming the edges (manually) (2 Edges) | Putting the piece away - taking another one | ||||||
| Sec | R | Sec | R | Sec | R | Sec | R | Sec | R | |
| Sample-1 | 3,8 | 100 | 10,2 | 100 | 13 | 105 | 30,4 | 95 | 1 | 100 |
| Sample-2 | 4,2 | 95 | 11 | 95 | 15 | 90 | 31 | 90 | 1 | 100 |
| Sample-3 | 5 | 95 | 10,6 | 100 | 14,5 | 100 | 29,4 | 100 | 2 | 90 |
| Sample-4 | 3,66 | 100 | 10,8 | 100 | 13,4 | 100 | 29 | 100 | 2,5 | 90 |
| Sample-5 | 3 | 105 | 12 | 90 | 13,9 | 100 | 30 | 100 | 2 | 90 |
| Sample-6 | 3,7 | 100 | 10,7 | 100 | 14 | 100 | 30,7 | 95 | 2 | 90 |
| Sample-7 | 2,9 | 110 | 11 | 100 | 14 | 100 | 29,8 | 100 | 1 | 100 |
| Sample-8 | 3,5 | 100 | 11 | 100 | 13,6 | 105 | 30 | 95 | 1 | 100 |
| Sample-9 | 3,7 | 100 | 10,2 | 100 | 15 | 90 | 32 | 90 | 1 | 100 |
| Sample-10 | 3,1 | 100 | 10 | 95 | 14,8 | 105 | 29,1 | 100 | 1 | 100 |
| Averages | 3,7 | 100,5 | 10,8 | 98,0 | 14 | 1 | 30,1 | 96,5 | 1,5 | 96,0 |
| Basic Time= Avg Time × Avg Rating 100 | 3,7 | 10,5 | 14,0 | 29,1 | 1,4 | |||||
| Total Basic Time | 58,7 | |||||||||
| Relaxation Allowance (%4) | 2,35 | |||||||||
| Unavoidable Delays (%7) | 4,11 | |||||||||
| STANDARD TIME (sec) | 65,2 | |||||||||
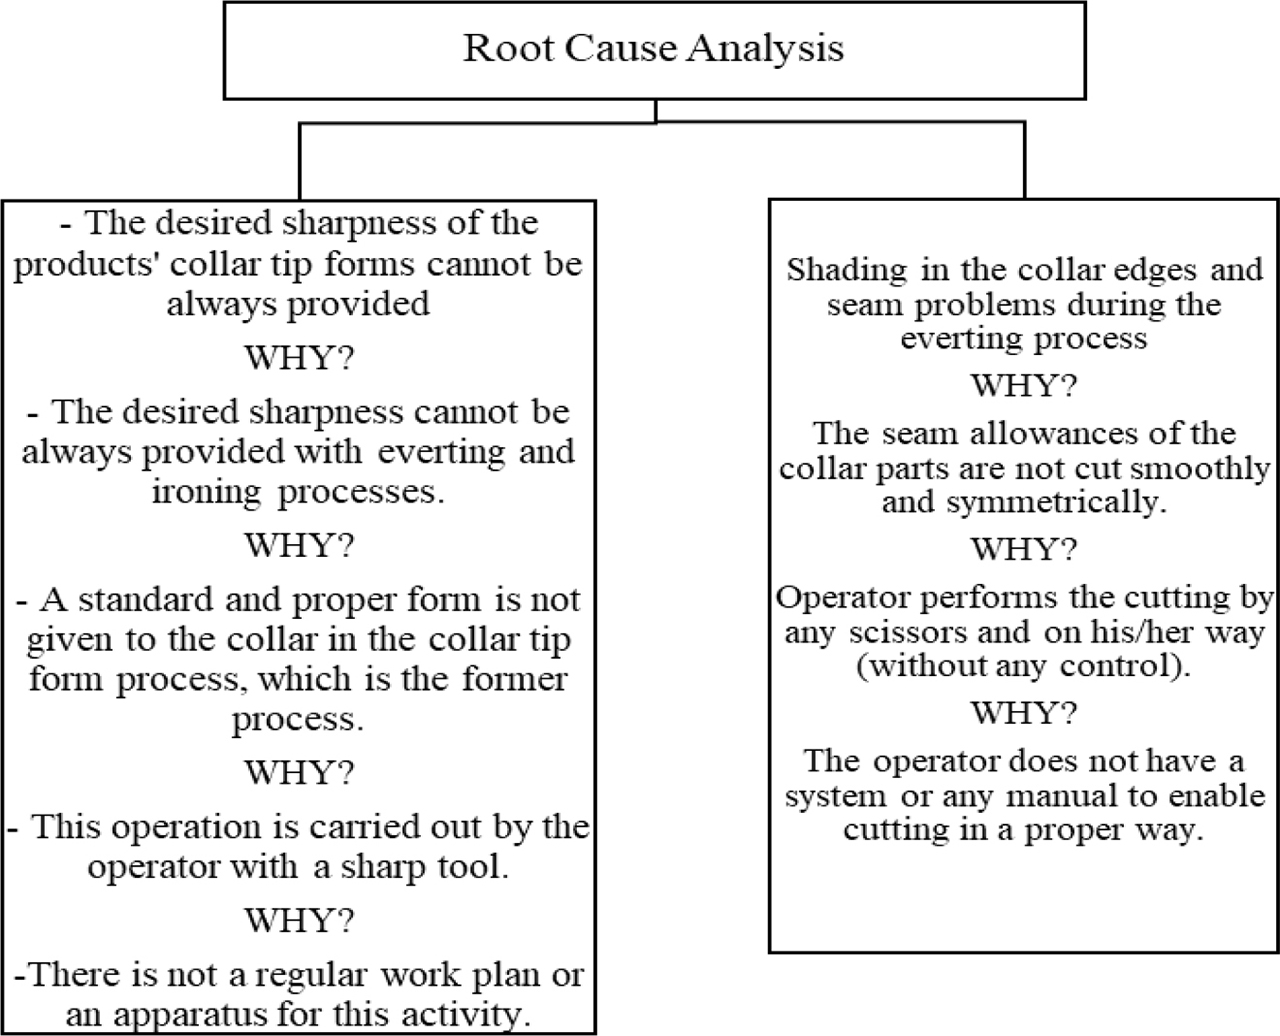
Fig. 10
Root cause analysis
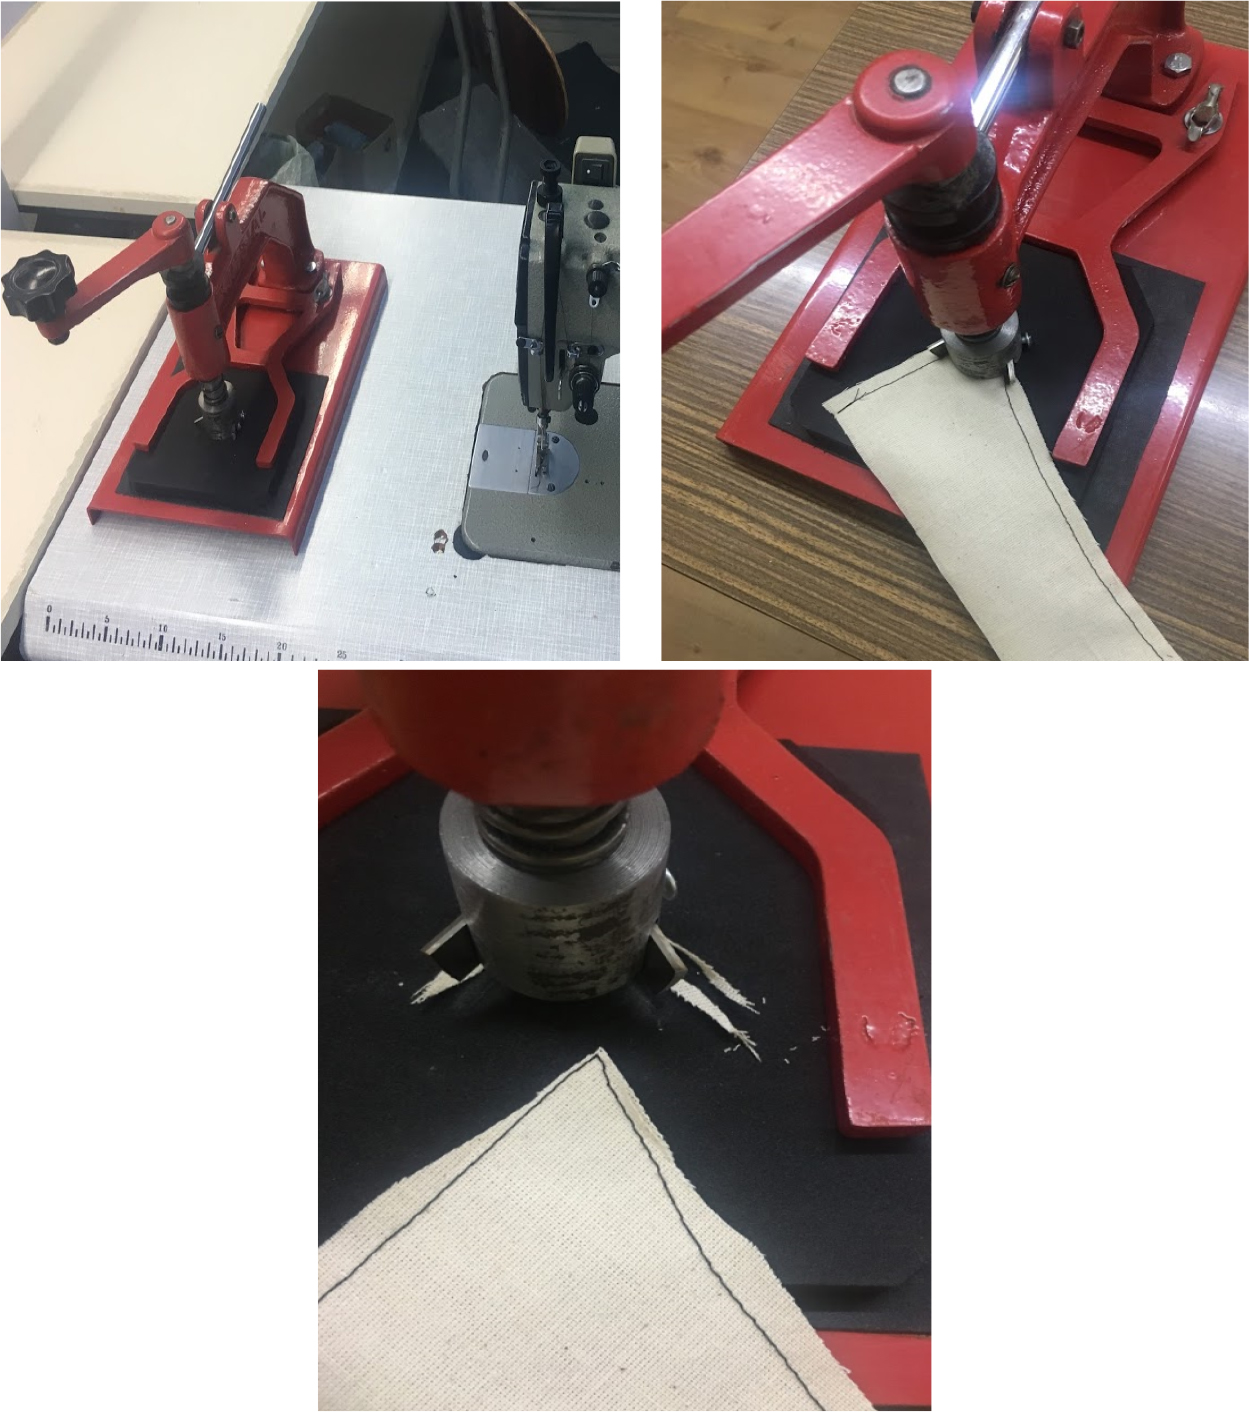
Fig. 11
Cutting apparatus

Fig. 12
Everting apparatus
Table 4
Records obtained by processes with the apparatus
| Collar Forming Records | ||||||||||
|---|---|---|---|---|---|---|---|---|---|---|
| With the Apparatus | ||||||||||
| Taking a piece - putting under the needle | Sewing | Cutting (the seam allowance) | Turn inside out - Forming the edges (with the apparatus) (2 Edges) | Putting the piece away - taking another one | ||||||
| Sec | R | Sec | R | Sec | R | Sec | R | Sec | R | |
| Sample-1 | 3,6 | 95 | 11 | 100 | 8,1 | 105 | 18,4 | 100 | 1,2 | 100 |
| Sample-2 | 3,2 | 100 | 11,2 | 110 | 7,5 | 105 | 18 | 100 | 1 | 100 |
| Sample-3 | 3,5 | 100 | 10,8 | 105 | 9 | 100 | 17,5 | 100 | 1,5 | 95 |
| Sample-4 | 3,6 | 95 | 10,9 | 105 | 7,3 | 100 | 17,7 | 95 | 1 | 100 |
| Sample-5 | 3,4 | 95 | 11,5 | 100 | 8,7 | 90 | 18,2 | 100 | 1,5 | 95 |
| Sample-6 | 3,4 | 100 | 11 | 100 | 9 | 90 | 18 | 100 | 1,4 | 95 |
| Sample-7 | 2,6 | 115 | 10,7 | 100 | 9 | 100 | 17,9 | 95 | 1,3 | 100 |
| Sample-8 | 4,2 | 90 | 10,8 | 100 | 8,7 | 90 | 17 | 95 | 1,2 | 100 |
| Sample-9 | 3,7 | 100 | 11,5 | 95 | 8,8 | 100 | 17,8 | 95 | 1,4 | 95 |
| Sample-10 | 3,9 | 100 | 10 | 110 | 9 | 100 | 19 | 90 | 1 | 100 |
| Averages | 3,5 | 99,0 | 10,9 | 102,5 | 8 | 5 | 18,0 | 97,0 | 1,3 | 98,0 |
| Basic Time= Avg Time × Avg Rating 100 | 3,5 | 11,2 | 8,3 | 17,4 | 1,2 | |||||
| Total Basic Time | 41,7 | |||||||||
| Relaxation Allowance (%4) | 1,67 | |||||||||
| Unavoidable Delays (%7) | 2,92 | |||||||||
| STANDARD TIME (sec) | 46,2 | |||||||||
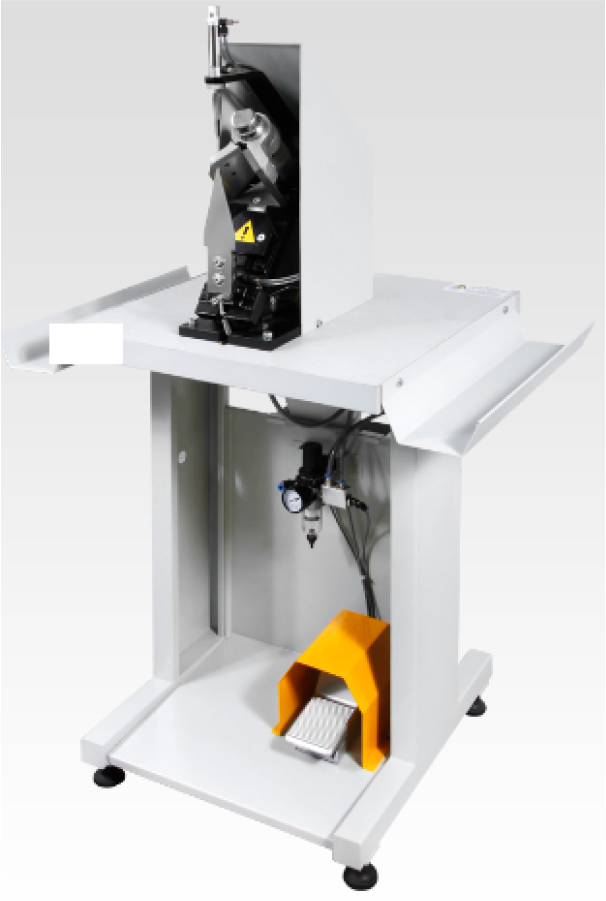
Fig. 13
Collar automat [9]
Table 5
Comparison of the techniques
| Std time-cutting process (sec) | Total std time (sec) | Price ($) | |
|---|---|---|---|
| Manually | 14,0 | 65,2 | - |
| Developed Apparatus | 8,3 | 46,2 | 84 |
| Automat | 7,9 | 24,6 | 2050 |