
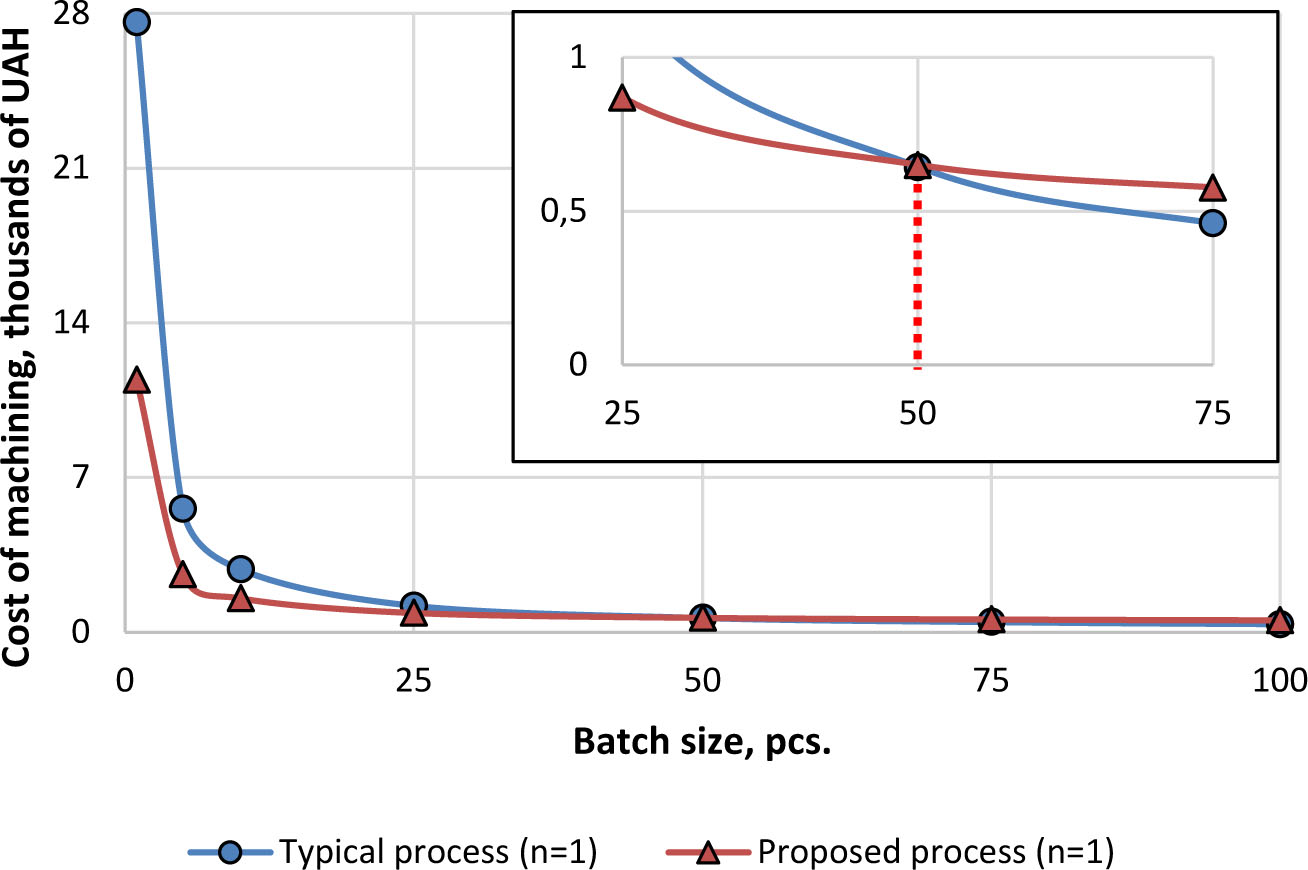
Fig. 1
Cost of machining parts depending on the batch size when machining one nomenclature of parts
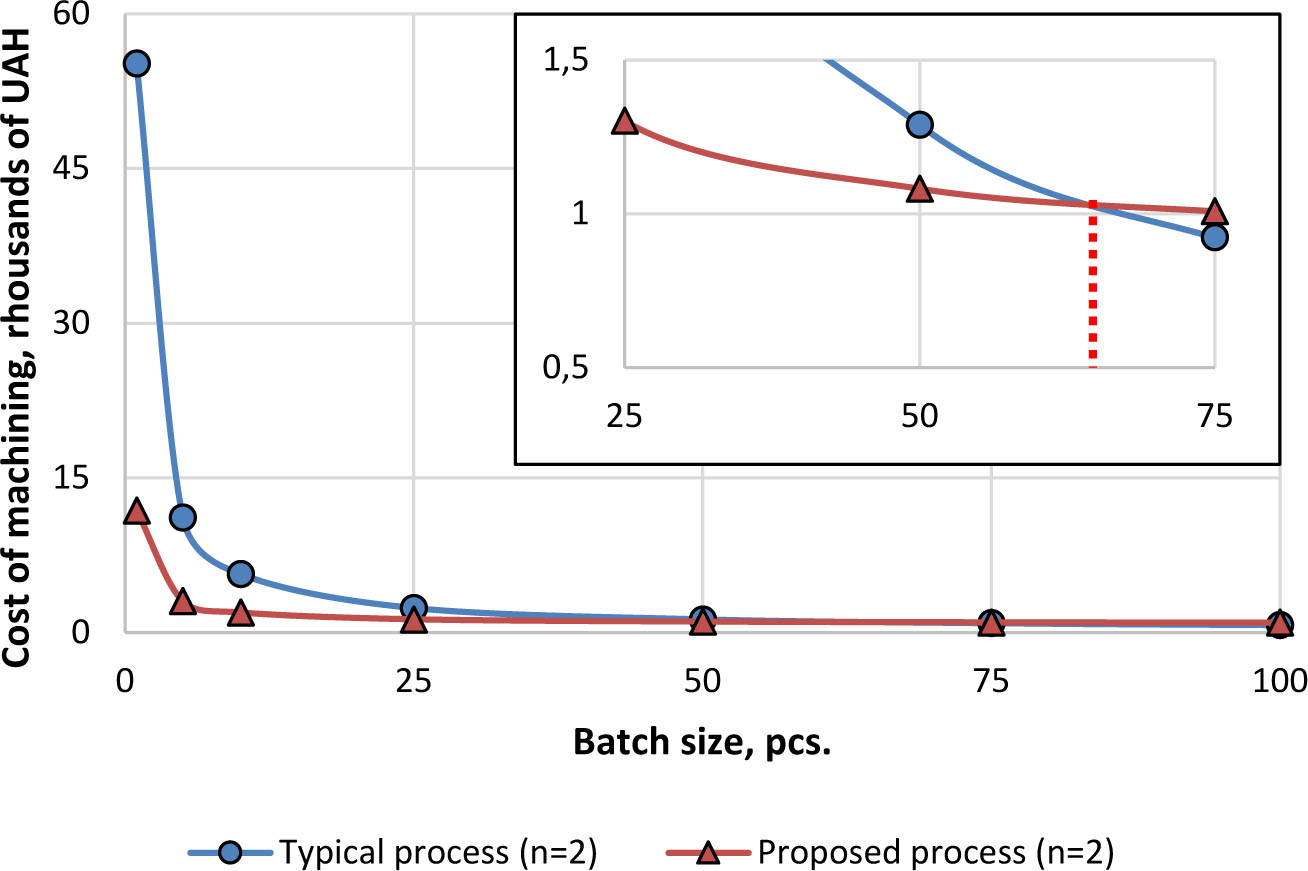
Fig. 2
Cost of machining parts depending on the batch size when machining the two nomenclatures of parts
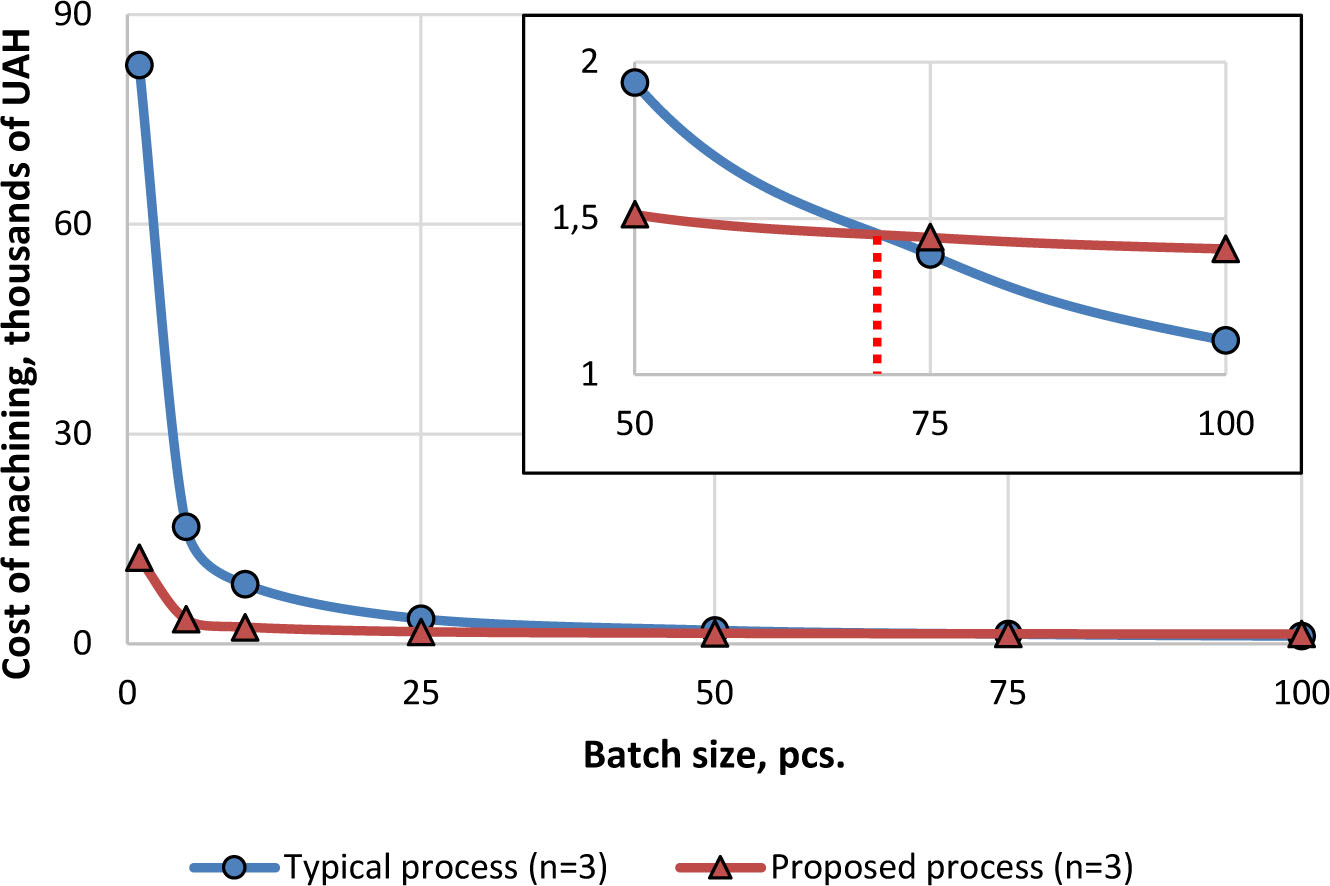
Fig. 3
Cost of machining parts depending on the batch size when machining the three nomenclatures of parts
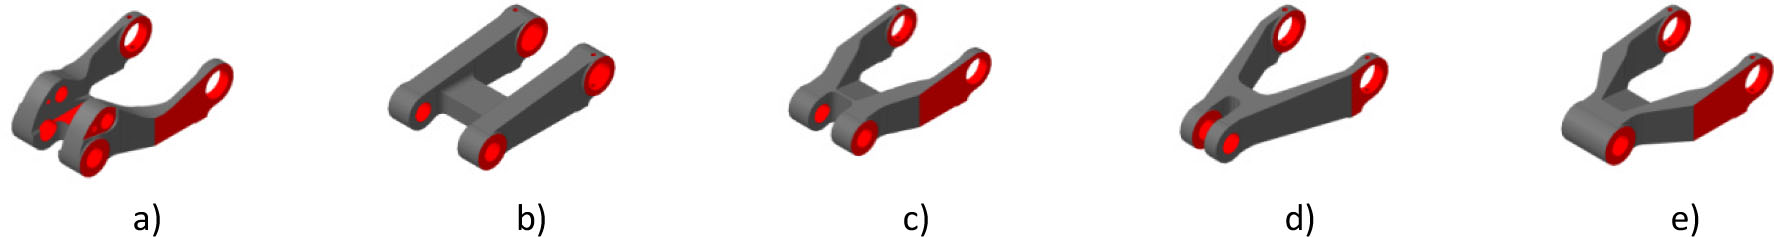
Fig. 4
Typical fork-type designs
Tab. 1
Comparison of the effectiveness of the proposed and typical manufacturing processes
| Fork-type design (according toFig. 4) | Name and code of the part | Batch size, pcs. | Manufacturing process | Cost, UAH | Comparative economic efficiency |
|---|---|---|---|---|---|
| a | Plug 99408076 | 30 | Typical | 1011.28 | 1.27 |
| Proposed | 797.38 | ||||
| b | Plug 3721-4511 | 40 | Typical | 782.12 | 1.05 |
| Proposed | 745.0 | ||||
| c | Plug 99408076-2 | 70 | Typical | 487.48 | 0.83 |
| Proposed | 587.86 | ||||
| d | Plug 73.02.34-01 | 100 | Typical | 369.62 | 0.68 |
| Proposed | 540.72 | ||||
| e | Plug 120.3-88.01.05 | 10 | Typical | 2844.62 | 1.86 |
| Proposed | 1530.72 | ||||
| a, b, c, d, e | Batch of parts | 250 | Typical | 5495.11 | 2.5 |
| Proposed | 2197.58 |